Products
Clad Plate Clad Pipe & Fittings Stainless Steel Products
Company
Materials & Grades Applications Quality & Standards About Us Contact Request a Quote
Home/Quality
Assurance

Quality & Standards

A clad product fails in service for one reason: a bond that was never fully bonded. Everything on this page exists to make sure that never leaves the works.
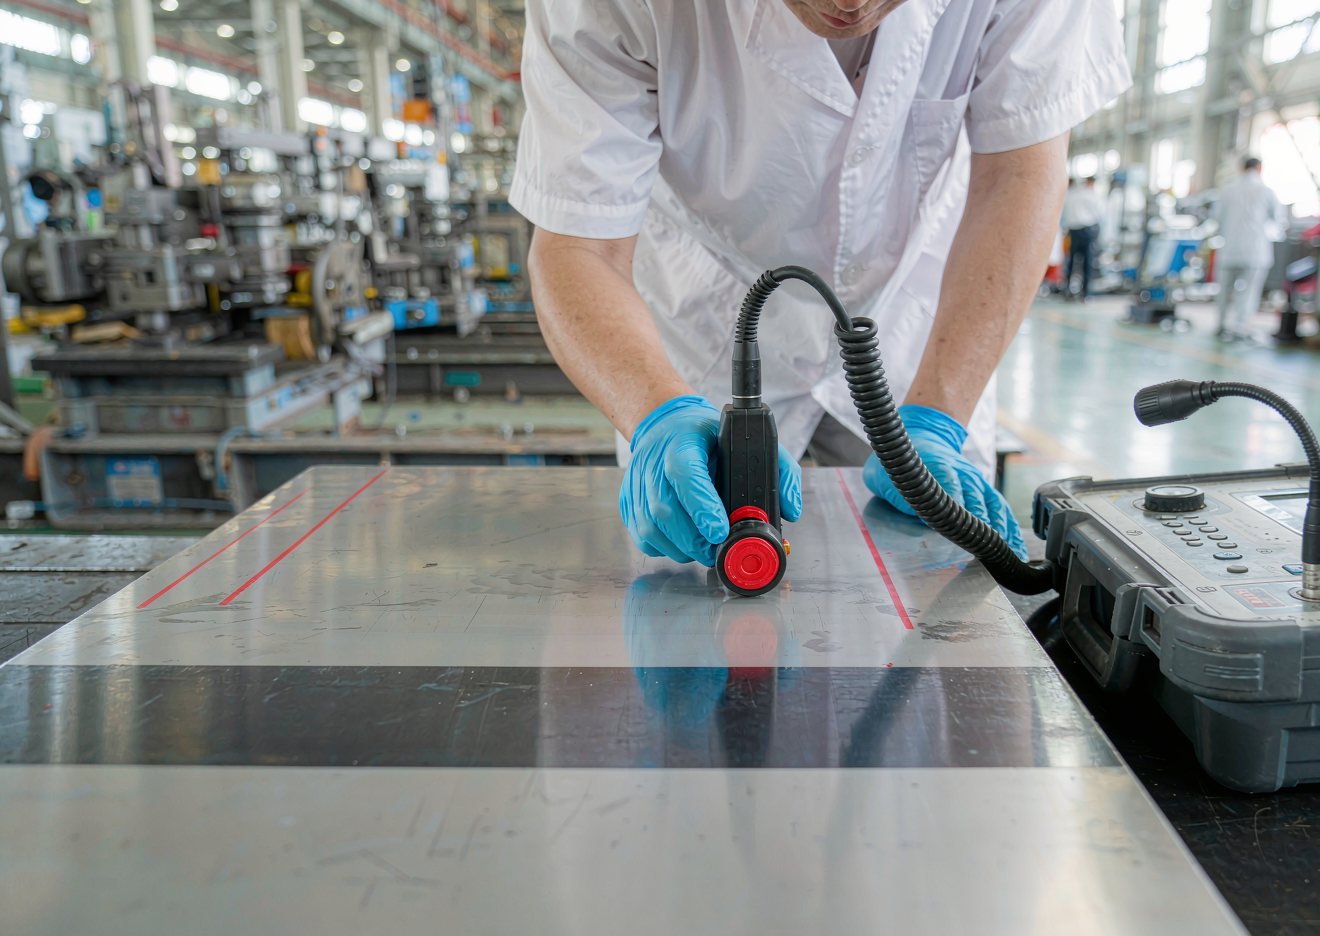
Technician performing ultrasonic bond testing on a clad plate 100% ultrasonic inspection
The principle

Test the whole surface,
not a sample of it.

Conventional inspection works by sampling — you test a plate from the batch and assume the rest is the same. That logic does not hold for a bonded interface. An unbonded area can be anywhere, on any plate, and it will not show up on the surface.

So every square metre of clad surface goes through ultrasonic inspection, and the scan map travels with the material certificate. You can see exactly where the inspection was done and what it found.

ISO 9001 : 2008 ISO 14001 : 2004 PED 97/23/EC TS Pressure Piping EN 10204 3.1 / 3.2
Acceptance criteria we hold to
Ultrasonic coverage100% of clad area
Bonding rate≥99.5% per plate
Single unbonded areanot permitted
Bond shear strength≥210 MPa
Side bend180°, no separation
Delamination at bendnone permitted
Thickness toleranceto order standard
Surface defect levelto order standard

Criteria follow the standard the order is placed against — GB/T 8165, ASTM A263 / A264 / A265, JIS G3601, EN or API 5LD. Where our internal limit is tighter than the standard, the tighter limit applies.
Process control

Seven gates between order and shipment

GATE 01
Incoming material
Base plate and cladding plate verified against the mill certificate: grade, heat number, dimensions and surface condition.
GATE 02
Surface preparation
Both mating surfaces ground clean and flat. Any contamination here becomes an unbonded area later.
GATE 03
Bonding
Explosion or hot-roll bonding to a qualified, recorded procedure with the charge and stand-off parameters logged.
GATE 04
Heat treatment
Normalising or annealing as required by the base steel and the applicable standard, with chart record.
GATE 05
100% ultrasonic test
Full-area scan for unbonded areas, with a map retained against the plate or pipe number.
GATE 06
Destructive tests
Shear, tensile, side bend, impact and metallography on samples taken from the same production lot.
GATE 07
Final & documentation
Dimensional check, marking, surface protection, and issue of the material test certificate.
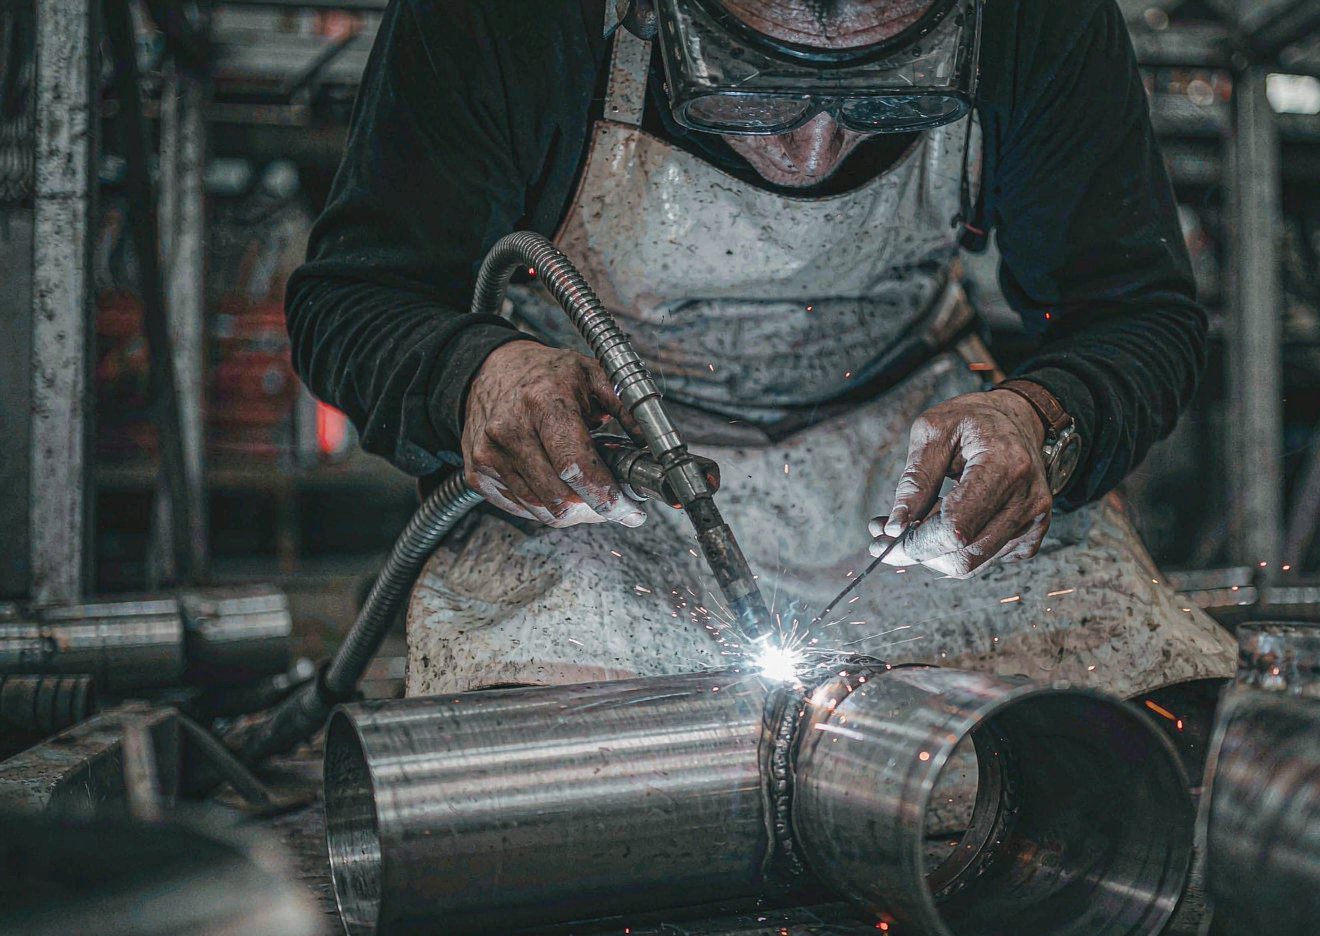
Welding a clad steel joint Welding & fabrication support
Test methods

What we test, how, and why

TestMethod / standardAcceptanceWhy it matters
Ultrasonic bond test GB/T 7734 · ASTM A578 · API 5LD Annex 100% coverage; no unbonded area The only way to find a bond that looks fine but is not bonded.
Shear strength GB/T 6396 · ASTM A264 ≥210 MPa typical Quantifies the interface strength that keeps the cladding in place under load.
Side bend GB/T 6396 · ASTM A263 / A264 180° with no separation Proves the bond survives the forming operations your shop will perform.
Tensile test ASTM E8 / E8M to the base steel grade Confirms the composite wall has the strength the design assumed.
Impact test ASTM E23, Charpy V-notch to project requirement Specified for low-temperature and offshore service where toughness is critical.
Hardness ASTM E10 / E18 · NACE MR0175 to sour service limit Hardness limits control susceptibility to sulphide stress cracking.
Metallography Microscopic examination of the bond line continuous, wave-form interface Shows the bond is metallurgical and free of inclusions or oxide films.
PMI XRF or OES positive material identification matches the certificate Confirms the alloy actually delivered is the alloy ordered.
Chemical analysis Spectrometric analysis of the heat within grade range The basis of the material test certificate.
Radiography / UT of welds ASTM E94 / E164 / E213 to the applicable weld standard For welded pipe seams, prefabricated spools and fabricated vessels.
Eddy current ASTM E426 no relevant indication Standard for heat exchanger and instrumentation tube.
Hydrostatic test to the applicable pipe or vessel standard held without leak or deformation Confirms the finished component holds pressure before it ships.
Independent verification

Your inspector is welcome

We would rather you verified the material yourself than took our word for it. Third-party inspection is routine, not exceptional.

Nominated inspection bodies
SGS, Bureau Veritas, TÜV, Intertek, Cotecna and most major inspection agencies can attend at the production stage you nominate — pre-bonding, post-bonding, post-UT or pre-shipment. Costs are passed through at cost.
Witnessed testing
Your representative or your agency's surveyor can witness the shear, bend and ultrasonic tests in person. Test samples are reserved for the purpose and identified before the run.
EN 10204 3.2 certificates
Where the project requires an independent signature on the material certificate, we can issue 3.2 instead of 3.1, with the inspection body countersigning the results against the heat number.
Documentation

What travels with the goods

A shipment with incomplete paperwork sits in a customs yard. Everything below is prepared as standard, not on request.

DOC
Material test certificate — EN 10204 3.1
Chemical composition, mechanical properties, heat number and, for clad products, the bond shear and ultrasonic results. Signed by the mill's authorised inspector.
DOC
Inspection reports
Ultrasonic scan report, dimensional record, hardness and PMI results, radiographic films or digital records for welds, and hydrostatic test record where applicable.
DOC
Export documents
Packing list, commercial invoice, bill of lading, certificate of origin (Form E / RCEP where applicable), marine insurance certificate and any buyer-nominated inspection release note.
DOC
Technical documents
Recommended welding procedure (WPS/PQR on request), handling and storage guidance, and the surface protection specification for the voyage.
Standards portfolio
Clad plateGB/T 8165
 ASTM A263 / A264 / A265
 ASME SA-263 / SA-264 / SA-265
 JIS G3601
 EN 1110
Clad pipeAPI 5LD
 GB/T 31940
 SY/T 6623
 ASTM A928
 DNV-OS-F101
Stainless plateASTM A240 / A480 · EN 10088-2
Stainless pipeASTM A312 / A213 / A269 · EN 10216-5
Duplex pipeASTM A790 / A789
Fittings & flangesASTM A403 / A815 / A182 · EN 1092-1
BarASTM A276 / A479 · EN 10272
Sour serviceNACE MR0175 / ISO 15156
Common questions

Quality questions we get asked

Under GB/T 8165 and ASTM A263 / A264 the requirement is normally a bonding rate of at least 99% of the tested area, with no single unbonded area exceeding the limit set by the standard or by your specification. We work to 99.5% or better per plate and do not accept a discrete unbonded area anywhere on the clad surface. The ultrasonic scan map is kept against the plate number so the result is auditable.
The side bend test is the direct answer. A strip is bent through 180° with the cladding on the tension side, and acceptance is that there is no separation, cracking or delamination at the interface. If the bond survives a 180° bend, it will survive the radii your shop will roll or press it to.
Yes. The standard minimum for clad plate is generally quoted at 210 MPa shear, and API 5LD sets a floor of 137.8 MPa for clad and lined pipe. If your project calls for a different figure, tell us and it becomes an acceptance criterion on your certificate.
Every heat is identified by PMI and spectrometric analysis before it is processed, and PMI is repeated on finished parts where the project requires it. The certificate is issued against the actual heat number, and we can arrange for a third party to countersign it as an EN 10204 3.2 if your client insists.
It does not ship. A plate that fails the ultrasonic or shear criteria is quarantined, the cause is recorded, and the material is either reworked to a qualified procedure and re-tested or rejected outright. You will see the outcome in the release note — we do not quietly substitute a borderline plate into a shipment.
Within reason, yes. Send us the buyer's documentation requirement — the nozzle schedule, the ITP, the certificate template, the marking instruction — and we will confirm what we can meet before the order is placed, not after.
Audit us

Ask for the certificates
before you place the order.

We will send a sample material test certificate, an ultrasonic scan report and a typical inspection and test plan for the product you are buying. Judge the paperwork first, then the price.
Mr. Cui — Sales Manager
+86 158 5280 5117
sales@xinleisteel.com